Printed from Kezuriba (kezuriba.net/en/troubles/tap-tearing/)
Thread is torn or galled
Tapping Tapping
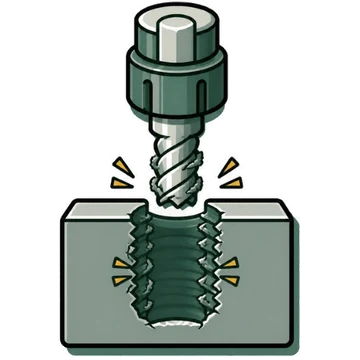
Check first
- Poor chip evacuation or clogging
- Welding to the tap
- Insufficient sharpness, or rake angle unsuited to the workpiece material
Try first
- In a synchronized feed setup, evacuate chips with step machining
- Reduce the cutting speed
- Use a sharp tap suited to the workpiece material (e.g. for aluminum)
?Likely causes
- Welding to the tapOne maker[1][2][3]
- Insufficient sharpness, or rake angle unsuited to the workpiece materialOne maker[3][2][1]
- Poor chip evacuation or cloggingAgreed by 2+ makers[1][2][3][4]
- Poor feed (lead) or axis runoutOne maker[1]
- Tap drill hole is work hardened, tilted, or too smallOne maker[1][2]
- Variation in workpiece material, hardness, or structureOne maker[1]
✓Fixes
Cutting conditions
- In a synchronized feed setup, evacuate chips with step machiningOne maker[3]
- Reduce the cutting speedOne maker[1][2]
Tool
- Use a sharp tap suited to the workpiece material (e.g. for aluminum)One maker[3][1][2]
- Use a surface-treated tap such as TiNOne maker[1][2]
- For horizontal machining, use a low-helix spiral tap to prevent chips from wrapping around itOne maker[4]
Setup
Coolant
▦Notes by material
- Aluminum castings (AC4CT6, etc.): Tearing is caused by one of insufficient sharpness, poor chip evacuation, or insufficient lubrication. Choose the countermeasure according to the cause[3]
↔Related problems
📚Sources
Causes and fixes are summarized in our own words from cutting-tool makers’ troubleshooting guides and technical data. “Agreed by 2+ makers” means two or more makers say the same thing.
- OSG — Tool Communication Series No.6 Taps, "12. Troubleshooting in tapping operations," pp. 59-62 osg.co.jp
- OSG — Series No.34 High-speed synchro taps, "8. Troubles and countermeasures," pp. 28-29 osg.co.jp
- OSG — Torn surface when machining aluminum faq.osg.co.jp
- Yamawa — Helpful Tips No.109: Chip control for SP taps in horizontal machining yamawa.com