Printed from Kezuriba (kezuriba.net/en/troubles/rolltap-entry-burr/)
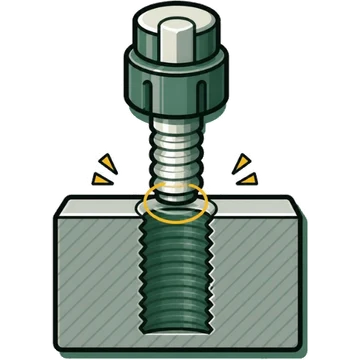
Burr or raised material at the entrance with a form (roll) tap
Tapping Tapping
Check first
- Form tapping deforms the material plastically, so material rises toward the entrance
Try first
- Chamfer the tap drill hole entrance
- Use a smaller chamfer angle (e.g. 90° to 60°, recommended 60-70°) and a larger chamfer diameter (for 120°, tap outer diameter + 2P)
?Likely causes
✓Fixes
Setup
↔Related problems
📚Sources
Causes and fixes are summarized in our own words from cutting-tool makers’ troubleshooting guides and technical data. “Agreed by 2+ makers” means two or more makers say the same thing.
- OSG — How to suppress burrs at the hole entrance when using a form tap faq.osg.co.jp
- Yamawa — Helpful Tips No.170: Countermeasures for entrance burrs on internal threads made with form taps yamawa.com