Centering with a dial indicator: four-jaw chuck, bores and bosses on a machining center, and the tailstock, by moving “half the runout”
The trick is to move just half the runout, not all of it. And bores and bosses go opposite ways!
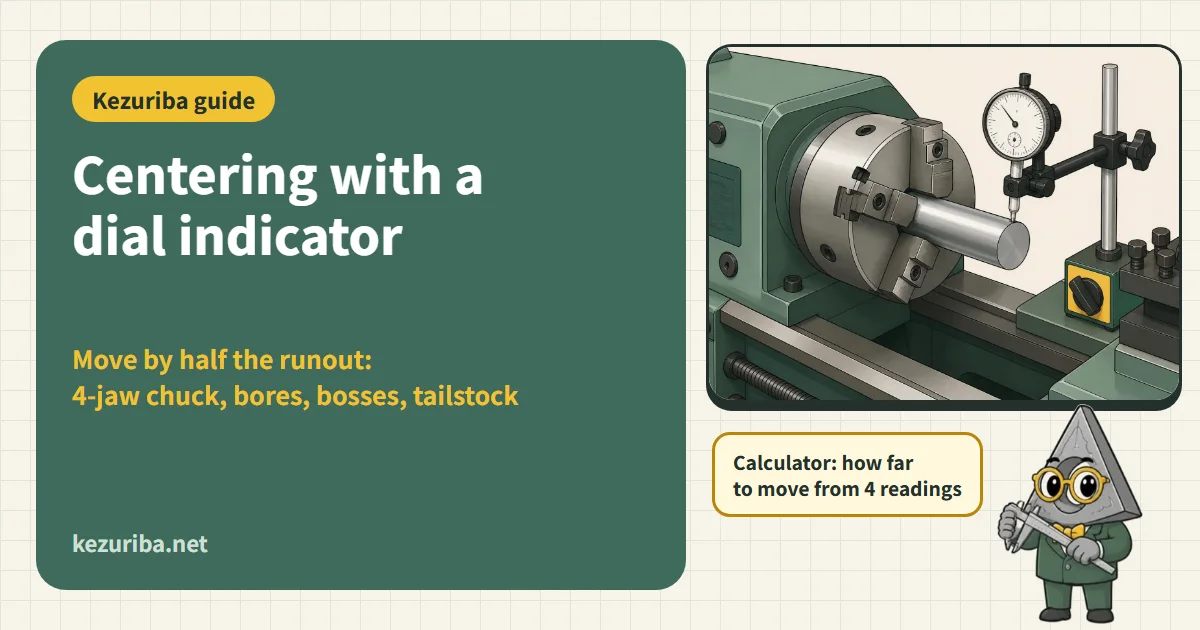
A round bar gripped in a four-jaw chuck on a lathe, a bore in a part sitting on a machining center table: before cutting, you line its center up exactly with the machine’s center of rotation (the spindle center). That job is centering (indicating in). If it’s off, the turned diameter won’t line up with the original bore, and you’ll miss the coaxiality or runout tolerance. This article sums up centering with a dial indicator and a dial test indicator in one idea, “move by half the runout you read while rotating,” and explains the steps for a four-jaw chuck, bores and bosses on a machining center, and the tailstock with diagrams and a calculator.
The idea: move by “half” the runout
In centering, you keep the indicator on the outside surface (or the bore wall), rotate the spindle and read how far the needle swings. The runout on the outside surface (max − min) is twice the center offset (eccentricity). So if you move the work (or the spindle) by half the runout, the centers line up. The idea is the same whether you are centering in a four-jaw chuck, finding the center of a bore on a machining center, or aligning the tailstock.
Aim for the “midpoint” of the readingsIf two opposite readings are 0.12 and 0.02, the difference is 0.10 and the center offset is 0.05. Move the work until the needle reads 0.07 (midway between the two readings) on the side that read high, and the opposite side will read 0.07 too, so the difference becomes 0. The trick is to set it to the midway value, not to zero on the dial.
Not all of the runout is center offset, though. Bumps in mill scale or a cast surface, and the roundness error of the work itself, also show up as runout. The runout you read while rotating includes both center offset and form error[11]. Center offset gives one peak and one valley per revolution (the wave in the diagram above), while form error often gives several peaks per revolution, so watch how the needle moves to tell them apart. For centering, the basic rule is to indicate on a clean surface, such as a finished or machined one.
Setting up the indicator: dial indicator and dial test indicator
| Dial indicator (plunger type) | Dial test indicator (lever type) | |
|---|---|---|
| Best for | Places you can contact straight on, such as OD runout on a lathe or aligning the tailstock | Bore walls, sweeping with it mounted in the spindle on a machining center, tight spots |
| How to set it | Keep the plunger at right angles to the surface. If it tilts, the reading won’t match the actual displacement[1][2] | Set the stylus nearly parallel to the surface (keep the angle θ as small as possible)[1][4] |
| If angled | — | The reading comes out larger than the actual displacement. Actual value = reading × cos θ[1][4] |
| Mounting | Overtightening the stem makes the plunger stick[1] | Use a rigid holder, with the stylus as close as possible to where the stand holds it (a long reach deflects)[4][8] |
- Preload slightly, then zero: Push the stylus in a little while it is touching, then set the dial, so it never lifts off and leaves spots you can’t read
- Read the needle from straight on: Looking from an angle causes misreads. The lathe event of the National Skills Competition (Japan) also lists “turn the spindle slowly while looking from directly above” as a step[5]
- Rotate slowly: Turn the spindle by hand or at very low speed. Too fast and the needle bounces, so you miss the peaks and valleys
Dial test indicator angle and correction factor
| Angle θ | 5° | 10° | 15° | 30° | 45° | 60° |
|---|---|---|---|---|---|---|
| cos θ | 0.996 | 0.985 | 0.966 | 0.866 | 0.707 | 0.500 |
The correction is “actual value = reading × cos θ,” and the Japan Precision Measuring Instruments Manufacturers Association’s guide gives the table above[4]. A measuring instrument maker’s guide gives the example of a reading of 0.002 mm at θ = 30°: 0.002 × 0.87 = 0.00174 mm[1][8]. Below 10°, the effect of θ is considered negligible (cos 10° = 0.985, a difference of about 1.5%)[7]. This error is specific to the dial test indicator, whose stylus moves in an arc; the maker explains that an indicator with a lever contact that converts the stylus motion into straight-line motion is not affected by the angle[3].
In centering, the “zero point” doesn’t shiftIf the angle θ stays the same, every reading is simply inflated by the same ratio (cos θ), so the conclusion of making the two readings equal (difference 0) doesn’t change. But when you “move by half the difference,” the inflated reading makes you overshoot, so it takes a few passes to close in. Enter θ in the calculator below and it corrects for it, giving the actual offset (mm). To calculate only the angle correction, you can also use the calculator on the dial test indicator page.
Lathe: centering in a four-jaw chuck
A four-jaw (independent) chuck lets you move each of its 4 jaws separately, so it can hold off-center work and can also center round bar very accurately. The Ministry of Health, Labour and Welfare’s manual for the lathe event defines centering as “making the machine spindle’s center of rotation coincide with the axis of the workpiece being machined,” and explains that it is done by repeatedly loosening and tightening the four jaws[5].
- Grip with the jaws evenly placed: Use the concentric rings on the chuck face as a guide to set the 4 jaws at about the same position, and put protective pads on the jaws if you don’t want to mark a finished surface. Tighten as evenly as you can while watching the runout[5]
- Set the indicator and zero it: Mount the stand on the tool post or carriage and contact the outside surface from directly above (or from the side at center height). Preload slightly, then zero the dial
- Bring each opposite pair to the midpoint: Steps ①–⑤ in the diagram above. Tighten the jaw on the high side and loosen the jaw on the low side (loosen first, then tighten)[11]. If the high spot is between two jaws, tighten the two adjacent jaws on the high side and loosen the two on the opposite side
- Set the other pair too: Turn 90° and do the same with the other 2 jaws. Moving one pair throws the other off a little, so alternate between the 2 pairs 2–3 times
- Final-tighten and check: Final-tighten a little at a time, alternating between opposite pairs[11]. Finally, turn it once more and read the runout; if it has shifted, redo just that pair. A thin-walled part that is overtightened gets cut while distorted, and once released it shows as many high spots as there are jaws[11]
In the lathe event of the National Skills Competition (Japan), competitors center the work about 50 times, and top competitors reportedly need only 2–3 minutes each time. The manual says skill at this job does more than anything else to cut working time[5]. Besides loosening and tightening the jaws, you can also tap the work over lightly. A study of a training simulator for centering found the tapping skill harder to learn than adjusting with clamping force in its trials[6]. A good way to practice is to close in with the jaws alone at first, then, once you’re used to it, nudge the work lightly with a plastic hammer.
Machining center: finding the center of a bore or boss
On a machining center or milling machine, to line the spindle up with the center of an existing bore (or a boss, i.e. a round projection), mount a dial test indicator in the spindle and turn it by hand, sweeping the bore wall (or the outside of a boss). Read at the 4 points +X, +Y, −X and −Y, and move the spindle (table) by half the difference between each opposite pair[12].
- Mount the indicator in the spindle: Mount the dial test indicator short and firm in an indicator holder or collet (a long arm deflects[4]). Make sure the spindle can be turned by hand
- Get roughly on center: By eye, jog to near the center of the bore (boss) with the manual pulse generator (handwheel), lower Z and touch the stylus to the surface. Preload slightly and zero the dial
- Read the two X points: Read at +X and −X and move X by half the difference (direction as in the diagram above). After moving, read the two points again to check
- Read the two Y points: Set +Y and −Y the same way
- Sweep a full turn to check: Finally, turn it one full revolution; if the needle barely moves, you’re done. Set that machine position as X and Y of the work coordinate system (G54, etc.). Even on a machine where the table moves, take machine +X as the direction the tool moves in +X relative to the work
Because the indicator turns with the spindle, the dial is hard to see when it’s on the far side (behind the spindle). Workarounds include setting up a mirror or remounting the indicator to face another way. There are also dedicated “coaxial indicators” whose dial stays facing you instead of turning, as well as edge finders and touch probes (on-machine measurement). Probes are fast and free of human misreading; when to use which is covered in the FAQ below.
Tailstock: aligning between centers
When turning a long shaft supported between centers or by the tailstock, if the tailstock center is offset sideways from the spindle center, the turned diameter comes out tapered (smaller at one end). If the tailstock is offset sideways by δ, the diameter at the tailstock end differs from that at the spindle end by 2δ.
- Align with a test bar: Mount a test bar of guaranteed straightness between centers, and read it at 2 points, the spindle end and the tailstock end, with an indicator fixed to the carriage. If both ends read zero, it’s aligned[11]. If the 2 points are roughly at the centers, the difference in readings is the tailstock’s sideways (radial) offset as is. If the distance l between the 2 points is shorter than the length L between centers, offset ≈ reading difference × L ÷ l
- Align by test cuts: Without a test bar, take a light cut at both ends of a scrap piece at the same depth of cut, and measure the diameters D₁ (spindle end) and D₂ (tailstock end) with a micrometer[11]. If you cut at both ends, tailstock offset ≈ (D₁ − D₂) ÷ 2 (× L ÷ l if the distance l between the 2 cuts is shorter than L). If D₂ is smaller, the tailstock is offset toward the tool (the front)
Here too, “half the diameter difference” is the center offset. Mix up diameter (both sides) and radius (one side) and you’ll move twice as far. A machine maker also publishes a procedure for checking tailstock alignment by turning the spindle 180° by hand and reading at 2 points, top and bottom[13].
Calculator: which way and how many mm to move, from 4 readings
Enter the readings taken at jaws 1–4 for a four-jaw chuck on a lathe, or at +X, +Y, −X and −Y on a machining center. For each opposite pair, you get the center offset, the direction to move and the target reading to set to. Enter readings as plus in the direction that pushes the needle in.
8 common mistakes
- Moving the full runout: The center offset is half the runout. Move the full amount and it ends up off by the same amount on the other side
- Getting the direction backwards for a bore vs. a boss: For a bore, move away from the high side; for a boss, toward it (diagram above)
- Setting the dial test indicator’s stylus at a steep angle: The larger the angle, the larger the reading, so you overshoot[1][4]
- A long or loose stand or arm: It deflects under the measuring force or its own weight, and the needle doesn’t move correctly[4]
- Losing it on final tightening: Even if it’s centered with light clamping, cranking just one jaw hard at the end pulls it off. Tighten all 4 evenly a little at a time, and read again after tightening
- Indicating on mill scale or a cast surface: You mistake surface bumps for eccentricity. Indicate on a machined surface, or tell them apart by the number of peaks per revolution
- Mixing up diameter and radius: A diameter difference measured with a micrometer is twice the center offset
- Reading the dial at an angle: Parallax between the needle and the dial causes misreads. Read from straight on[5]
Suspect the indicator itselfWhen a prefectural industrial research institute inspected 73 dial indicators from 6 local companies to JIS, about 38% failed, and 82% of the dial test indicators failed. The causes were put down to leaving them mounted on machine tools, so that chips and cutting oil got inside, and to gears wearing on one side from always using the same range[15] (a 1991 report). Before use, push the stylus and release it to check that it returns to 0[9], and send them out for regular inspection and calibration. How to check one is covered on the dial test indicator page.
FAQ
- How closely should I center it?
- Decide from the runout and coaxiality tolerances on the drawing, and stop once you’re well within the tolerance. Chasing it further only takes time. An indicator with a 0.01 mm graduation can’t be read finer than one graduation, so to align within a few µm, use a dial test indicator with a 0.002 mm or 0.001 mm graduation.
- Can I center work in a three-jaw chuck too?
- A three-jaw (scroll) chuck moves all 3 jaws together, so you can’t nudge one jaw at a time as with a four-jaw. A well-used three-jaw can be off center by about 0.05–0.25 mm, and one method described is to slip paper or thin shim between the high-side jaw and the work to shift it[11]. When you need accuracy, the reliable way is to machine (form) the soft jaws in place, then grip. Soft jaws lose accuracy when removed and refitted, so re-form them after refitting[14]. Some chucks also let you shift the chuck body with adjusting screws to dial out the runout.
- When should I use an edge finder or touch probe instead?
- An edge finder picks up a face and you add or subtract half its tip diameter; for a bore, you pick up both sides and take the midpoint. A touch probe measures automatically with a machine cycle, so it’s fast and free of human misreading. Sweeping with a dial indicator works on any machine whose spindle can be turned by hand, and its advantage is that you can also see out-of-roundness of the bore in the needle’s movement as you sweep[12].
- Should I use a dial test indicator or a plunger-type dial indicator?
- The plunger type suits places you can contact straight on from above, like the OD on a lathe; the dial test indicator suits bore walls and sweeping with it mounted in the spindle on a machining center. Don’t forget the angle correction with a dial test indicator.
- I want to learn how to read a dial indicator in the first place.
- Dial indicator and Dial test indicator (lever type) pages cover practice in reading the dial, the names of the parts, and how to inspect them.
Sources
- Mitutoyo: “Basics of Digimatic Indicators, Dial Indicators and Test Indicators” (in Japanese)
- Mitutoyo, “Quick Guide to Precision Measuring Instruments” (E4329)
- Mitutoyo: “Eliminating Sources of Measurement Error in Dial Test Indicators (Test Indicators)” (in Japanese)
- Japan Precision Measuring Instruments Manufacturers Association: “Dial Test Indicators” (explanation of JIS B 7533:2015, Annex F: precautions for use) (in Japanese)
- Ministry of Health, Labour and Welfare: “Manual for Developing Human Resources through Skills Competitions (Lathe)” (in Japanese)
- Hashimoto, Kato, Aoyado, Higuchi, Okawa: “Training of Centering Work on a Lathe with a Simulator,” Journal of the Japan Society for Precision Engineering 79(8), 779–783 (2013) (in Japanese)
- Mitutoyo, “Check Points for Measuring Instruments” (E12024)
- Mitutoyo, "Dial Test Indicator User’s Manual"No. 99MAG023A3
- Niigata Seiki: “Dial Test Indicator WTI Series Instruction Manual” (in Japanese)
- Nidec Motor Corporation, "Measuring Shaft Runout"
- U.S. Navy, “Machinery Repairman 3 & 2,” NAVEDTRA 12204 (lathe chapter: four-jaw, three-jaw, tailstock)
- Tormach, "Fab Lab Skill Builder: Swing Indicating, Part 1"
- Haas Automation, "ST - Tailstock Concentricity to Spindle Correction"
- Haas Factory Outlet, “Haas Lathe Setup and Operation” (training material; forming soft jaws)
- Oita Prefectural Industrial Research Institute: “Maintaining the Accuracy of Dial Indicators Used by Companies in the Prefecture” (1991) (in Japanese)
More articles
 NC
Lathe Multiple Repetitive Cycles: G71 (OD/ID Roughing) + G70 (Finishing), G72 (Facing), G73 (Pattern Repeating) and G76 (Threading)
 Industry
How a metalworking company can enter medical device parts machining: common parts and materials, market trends, major makers, the PMD Act, ISO 13485 and the hurdles
 Gears