Printed from Kezuriba (kezuriba.net/en/troubles/poor-surface-finish/)
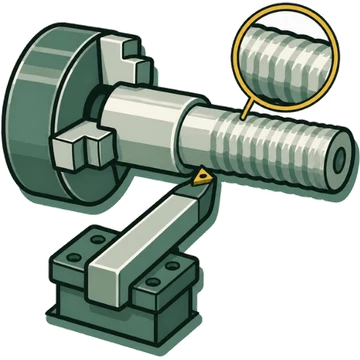
Rough, torn, or fuzzy finished surface
Turning and milling TurningMilling
Check first
- Built-up edge or welded material is on the cutting edge
- Chatter vibration is occurring
- Feed is large relative to the corner radius or wiper flat width (feed marks)
Try first
- Increase the cutting speed to prevent built-up edge and welding
- Reduce the feed (in face milling, keep the feed per revolution within the wiper flat width)
- Use a wiper insert or a larger corner radius
?Likely causes
- Built-up edge or welded material is on the cutting edgeAgreed by 2+ makers[1][2][3][4][5]
- Chatter vibration is occurringAgreed by 2+ makers[1][2][3][6][5]
- Feed is large relative to the corner radius or wiper flat width (feed marks)Agreed by 2+ makers[7][1][4][8][9]
- Tool wear or chipping is advancedAgreed by 2+ makers[2][4][9][10]
- Chips hit the machined surface or are being recutAgreed by 2+ makers[7][9][11][10]
- Runout of the tool or spindle, or uneven insert heightsAgreed by 2+ makers[1][4][11][9][6]
- Cutting speed is low (e.g. fuzzy surface on mild steel)Agreed by 2+ makers[9][2][3]
- Large boundary wear makes the machined surface fuzzyOne maker[7]
✓Fixes
Cutting conditions
- Increase the cutting speed to prevent built-up edge and weldingAgreed by 2+ makers[1][2][3][4][9][5]
- Reduce the feed (in face milling, keep the feed per revolution within the wiper flat width)Agreed by 2+ makers[7][1][4][8][9][11]
Tool
- Use a wiper insert or a larger corner radiusAgreed by 2+ makers[7][1][4][6][3]
- Use a sharp positive geometry with a large rake angle and small honingAgreed by 2+ makers[1][2][3]
- Use a grade with low affinity to the workpiece material (cermet or coated)Agreed by 2+ makers[7][1][2][4][3]
- Replace worn or chipped cutting edges earlyAgreed by 2+ makers[4][9]
Setup
- Reduce runout (align insert heights, and check spindle and holder runout)Agreed by 2+ makers[1][4][9][11][6]
- Direct chips away from the machined surface (select a chip breaker, use air blow)Agreed by 2+ makers[7][9][11][10]
Coolant
▦Notes by material
↔Related problems
📚Sources
Causes and fixes are summarized in our own words from cutting-tool makers’ troubleshooting guides and technical data. “Agreed by 2+ makers” means two or more makers say the same thing.
- Sandvik Coromant — Milling troubleshooting sandvik.coromant.com
- Tungaloy tungaloy.com
- Mitsubishi Materials — Turning troubleshooting mmc-carbide.com
- Tungaloy tungaloy.com
- Mitsubishi Materials — Advanced Turning: Troubleshooting mmc-carbide.com
- Mitsubishi Materials — Face milling troubleshooting mmc-carbide.com
- Sandvik Coromant — Troubleshooting in turning sandvik.coromant.com
- Tungaloy tungaloy.com
- OSG — Series No.8 End mills, Table 7.1 Troubleshooting, pp. 61-62 osg.co.jp
- Mitsubishi Materials — End milling troubleshooting mmc-carbide.com
- Mitsubishi Materials — End mills: troubleshooting mmc-carbide.com
- Mitsubishi Materials — Workpiece material applications: P series mmc-carbide.com
- Mitsubishi Materials — Workpiece material applications: N series mmc-carbide.com