Printed from Kezuriba (kezuriba.net/en/troubles/wall-deflection/)
Walls lean or are wavy (end milling)
Turning and milling Milling
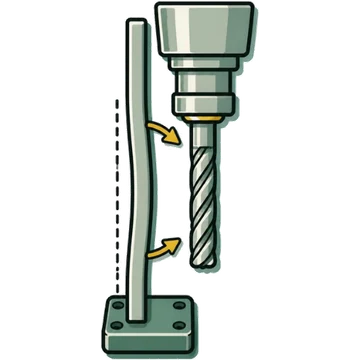
Check first
- Depth of cut or feed is large
- Insufficient tool rigidity or long overhang
- Tool wear is large
Try first
- Reduce the depth of cut and use step machining in the axial direction
- Reduce the feed per tooth
- Split into roughing, semi-finishing, and finishing, and reduce the finishing allowance
?Likely causes
✓Fixes
Cutting conditions
- Reduce the depth of cut and use step machining in the axial directionAgreed by 2+ makers[2][1][3]
- Reduce the feed per toothAgreed by 2+ makers[2][1][3]
- Split into roughing, semi-finishing, and finishing, and reduce the finishing allowanceAgreed by 2+ makers[2][4]
- Do the finishing pass with up millingOne maker[2]
Tool
↔Related problems
📚Sources
Causes and fixes are summarized in our own words from cutting-tool makers’ troubleshooting guides and technical data. “Agreed by 2+ makers” means two or more makers say the same thing.
- Mitsubishi Materials — End mills: troubleshooting mmc-carbide.com
- OSG — Series No.8 End mills, Table 7.1 Troubleshooting, pp. 61-62 osg.co.jp
- Mitsubishi Materials — End milling troubleshooting mmc-carbide.com
- Tungaloy tungaloy.com