Printed from Kezuriba (kezuriba.net/en/troubles/flatness/)
Poor flatness or parallelism (face milling)
Turning and milling Milling
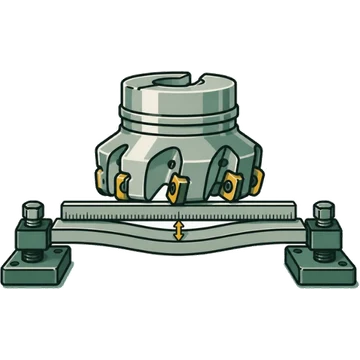
Check first
- Workpiece deflects
- Tool deflects
- Thrust force is large
Try first
- Reduce the feed and depth of cut
- Use a sharp cutting edge, a cutter with a small corner angle, and fewer teeth
- Increase tool and workpiece mounting rigidity
?Likely causes
✓Fixes
Cutting conditions
Tool
Setup
↔Related problems
📚Sources
Causes and fixes are summarized in our own words from cutting-tool makers’ troubleshooting guides and technical data. “Agreed by 2+ makers” means two or more makers say the same thing.
- Mitsubishi Materials — Face milling: Troubleshooting mmc-carbide.com
- Mitsubishi Materials — Face milling troubleshooting mmc-carbide.com